2025-12-20
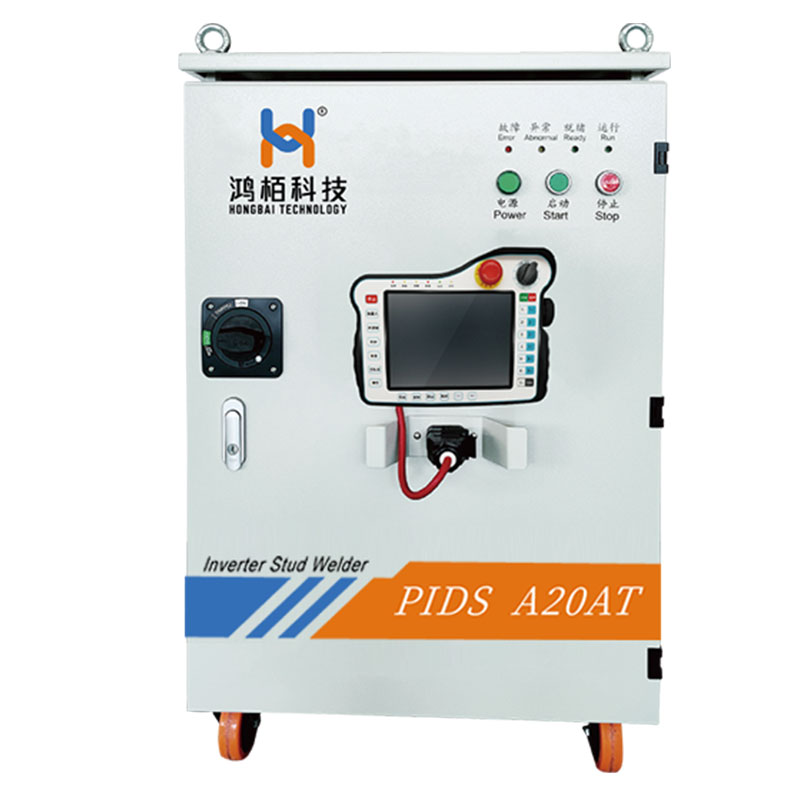
The welding system main unit adopts an ARM+FPGA system architecture, featuring the world’s most advanced 50kHz full-bridge soft switching, AC/DC output, 100K pure digital hardware current loop, pure digital control linear servo drive technology, and integrated information technology.
2026-09-08
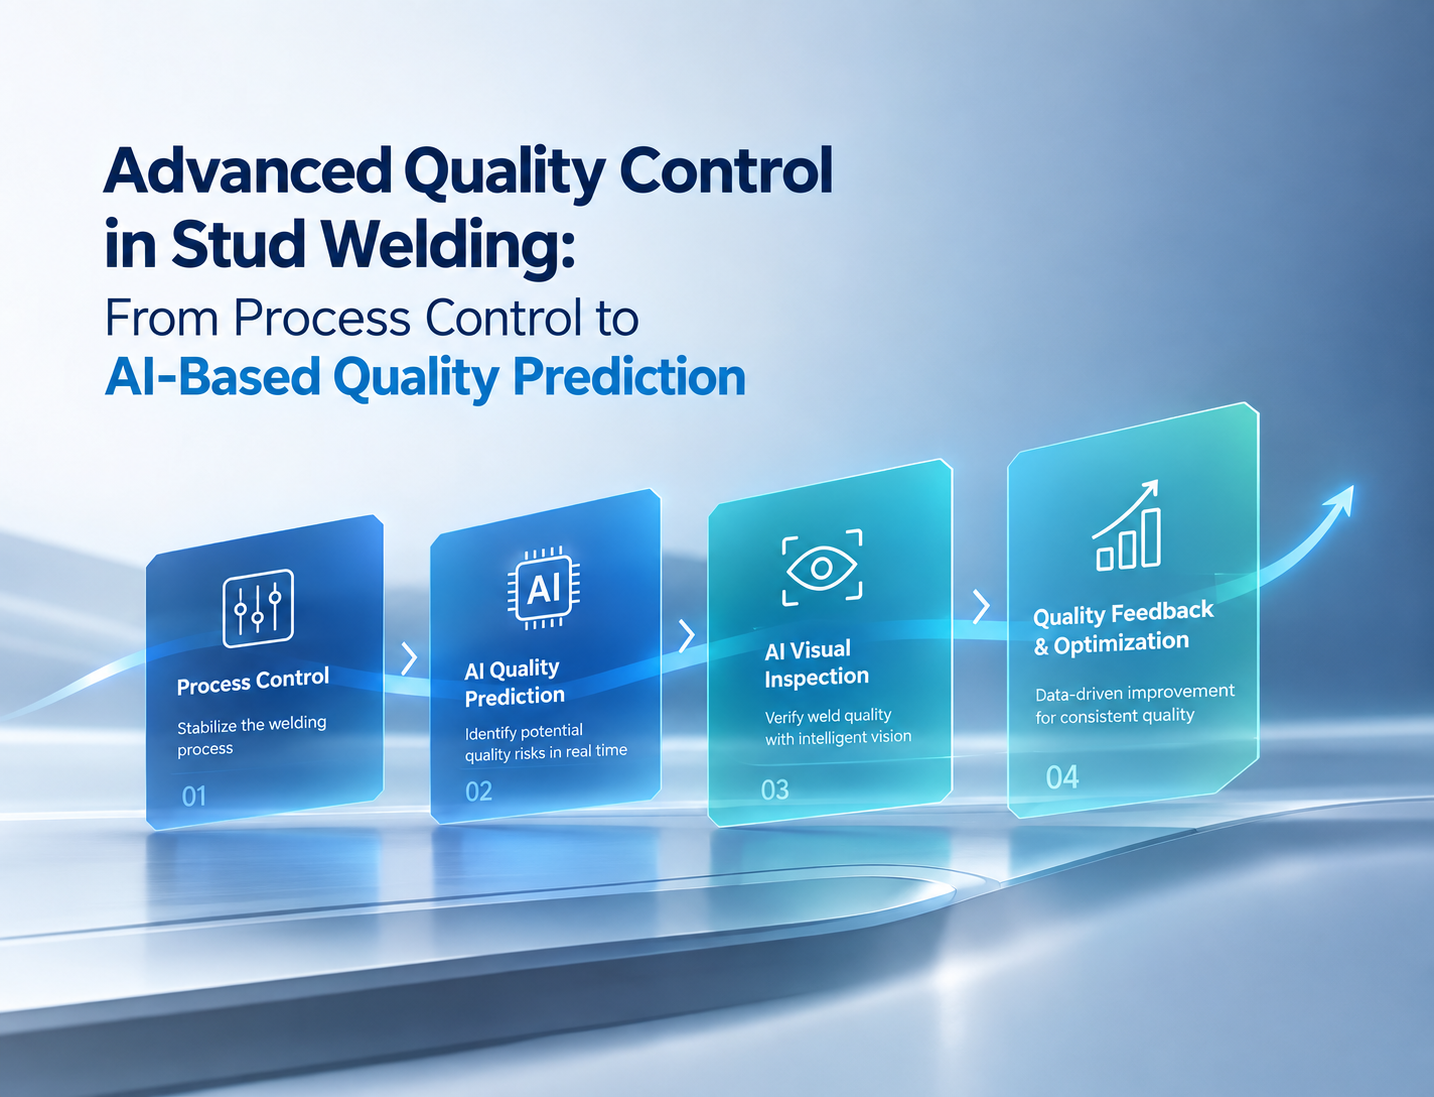
In stud welding production, the real challenge is often not whether a stud can be welded successfully, but whether it can be welded consistently and reliably over and over again. For a single stud, achieving a successful weld may not be particularly difficult. However, once stud welding is introduced into high-volume production environments such as automotive body-in-white, construction machinery, rail transportation, and sheet-metal manufacturing for home appliances, a single system may be required to perform thousands or even tens of thousands of welds continuously. At that point, weld quality is no longer determined simply by preset parameters such as weld current and weld time. Line voltage can fluctuate. The surface condition of the workpiece may vary due to oil contamination, oxidation, or coating differences. Pneumatic supply pressure may change. Equipment temperature may rise during extended operation. Different batches of studs may also vary in material properties and dimensional tolerances. Although these changes may appear minor, they can affect the arc condition, melting behavior, and final weld result within a welding cycle that takes place in milliseconds. For true high-volume manufacturing, therefore, the question is no longer simply: “Can this stud be welded successfully?” The more important question is: “When production conditions continuously change, how can the first stud and the last stud maintain as consistent a welding condition as possible?” This is exactly the challenge addressed by AQC2, Hongbai’s 2nd-Generation Active Quality Control technology, within the HEAS intelligent stud welding system. 1. From Parameter Execution to Active Control: A Changing Approach to Stud Weld Quality Traditional stud welding typically follows a straightforward sequence: Set Parameters → Perform Welding → Inspect After Welding Engineers set parameters such as weld current, weld time, and lift distance according to the workpiece material, stud specifications, and process requirements. The equipment then performs the weld…
2026-09-07
Shenzhen, China — September 2026 — Shenzhen Hongbai Technology Co., Ltd. has been recognized as one of the Top 100 Emerging Enterprises in Longgang District, following the announcement made at the 2026 Longgang Enterprise Service Conference. The conference was hosted by the CPC Longgang District Committee and the Longgang District Government. Hongbai Technology was selected for its strong innovation capabilities, solid technical expertise, and continued growth, marking another important recognition of the company’s development in Longgang and its more than 20 years of commitment to intelligent welding equipment. More Than 20 Years of Technology and Manufacturing Founded in 2003 and headquartered in Longgang District, Shenzhen, Hongbai Technology is a National High-Tech Enterprise and a National-Level Key “Little Giant” Enterprise, as well as a Guangdong Manufacturing Single Champion Enterprise and a standing council member of the China Welding Association. The company has also participated in national key scientific and technological research projects and National Torch Program projects. Hongbai Technology focuses on the R&D and manufacturing of intelligent equipment and customized industrial software, with capabilities covering the complete process from core technology development and precision manufacturing to system integration. With more than two decades of experience, the company has built particular expertise in automotive manufacturing and intelligent welding equipment, serving the evolving needs of modern manufacturing. Strong R&D and Engineering Capabilities Hongbai Technology currently has nearly 600 employees, with R&D personnel accounting for approximately 30% of its workforce. The company invests more than 15% of its annual sales revenue in R&D, continuously developing technologies for intelligent welding, automation, robotics, industrial software, and AI-enabled manufacturing. To date, Hongbai Technology has accumulated more than 200 patents and software copyrights across its domestic and international technology portfolio. The Guangdong Engineering Technology Research Center for Welding Equipment is also based at Hongbai Technology, further supporting the…
2026-09-01
1. Stud Welding in Sheet Metal Electrical Enclosure Manufacturing Stud welding is widely used for fastening applications in electrical enclosures, control cabinets, switchgear cabinets, distribution boxes, and other sheet metal structures. Compared with conventional nut welding, drilling and tapping, or mechanical fastening, stud welding allows a threaded stud or fastening element to be permanently attached directly to the sheet metal surface, reducing additional machining and assembly operations. Typical applications include grounding studs, mounting studs for circuit breakers and terminal blocks, busbar supports, cable management components, door hardware, and other internal cabinet components. In practical production, the selection of a sheet metal stud welding process depends mainly on sheet thickness, stud diameter, base material, required joint strength, surface condition, and the appearance requirements of the opposite side of the workpiece. For thin sheet metal electrical enclosures, minimizing distortion, discoloration, and visible marks on the reverse side can be particularly important. For structural components and grounding connections, weld strength and process consistency may take priority. Therefore, selecting stud welding equipment for electrical enclosures requires more than simply checking the welding current or stud diameter. The welding power source, stud welding gun, stud feeder, workholding system, and level of automation all need to be considered as part of the same process. 2. Capacitor Discharge and Drawn Arc Stud Welding 2.1 Capacitor Discharge Stud Welding Capacitor discharge (CD) stud welding stores electrical energy in capacitors and releases it over an extremely short welding cycle. Typical welding time is approximately 0.001–0.003 seconds, with peak current reaching approximately 5,000–10,000 A. Because the welding cycle is extremely short, heat input is concentrated around the weld area. This makes capacitor discharge stud welding particularly suitable for thin sheet metal and applications where backside appearance is important. Hongbai’s PFC Series capacitor discharge stud welding machines support stud diameters from…
2026-08-19
In July 2026, at the AMTS Shanghai International Automotive Manufacturing Technology & Material Show, Hongbai Technology made the global debut of its fully self-developed AI foundation-model-powered stud welding quality inspection system. It is also the world’s first quality management system integrating an AI foundation model specifically for stud welding applications. As AI foundation models rapidly transform industries worldwide, Hongbai Technology is bringing this transformation to the welding industry. After six generations of welding technology evolution, the company has consistently focused on the integration of data, algorithms, and real-world industrial scenarios, while addressing four fundamental challenges in industrial AI. Through the dual revolution of “Welding + AI,” Hongbai Technology is pioneering a new paradigm for stud welding quality management—moving from experience-driven quality control to data- and algorithm-driven intelligence. 1. Industry Challenges: Four Limitations of Traditional Quality Inspection 1.1 Fragmented and Heterogeneous Data In high-volume stud welding production, traditional quality management faces a series of systemic challenges. Fragmented and heterogeneous data: Quality records are often scattered across paper documents, PowerPoint files, Excel spreadsheets, welding equipment, and other systems, making data integration time-consuming and inefficient. 1.2 Slow Problem Detection and Response Quality issues may take up to four hours to be detected under periodic inspection. Once identified, the escalation and feedback process may require another 1–2 hours, while problem resolution can take up to 3.5 hours. In addition, compiling daily quality inspection reports can consume approximately 2.25 hours of labor every day. For high-volume automotive production, such delays increase the risk of quality issues escaping downstream and can lead to additional rework and production costs. 1.3 Manufacturing Knowledge Is Difficult to Capture and Reuse Root cause identification and corrective action often depend heavily on the experience of individual engineers and technicians. When critical welding knowledge remains primarily within individual experts, it becomes difficult…
2026-08-06
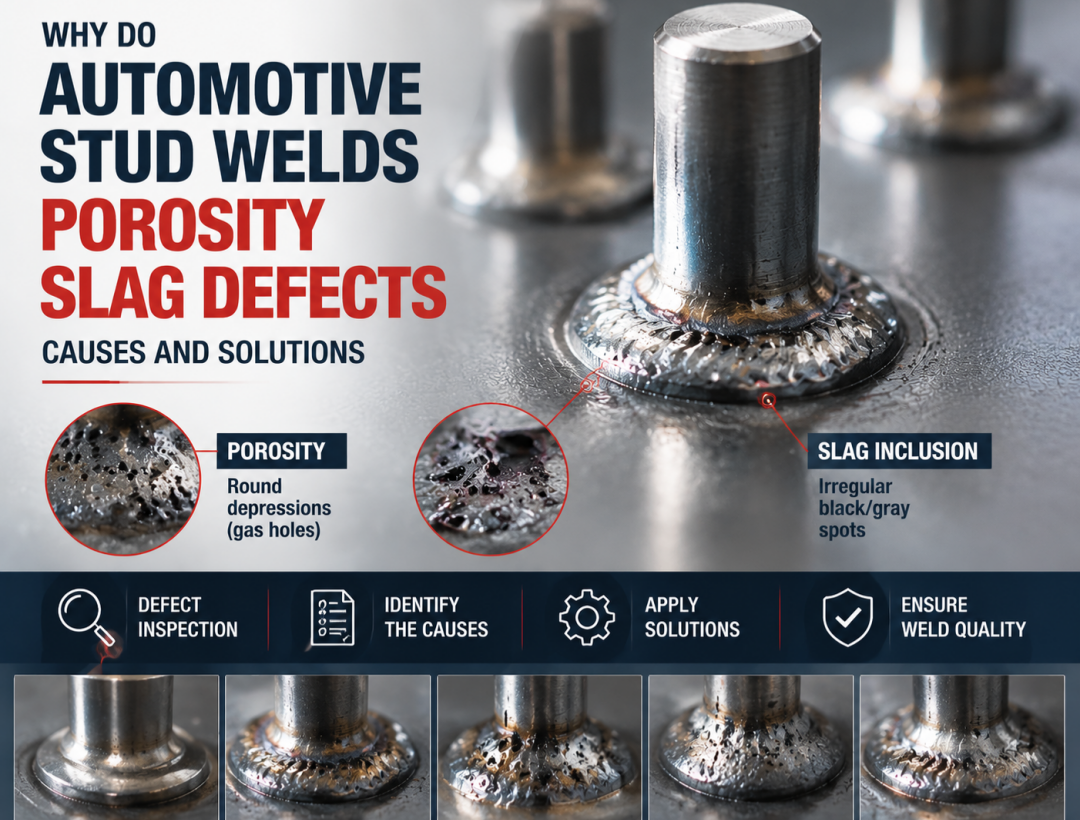
Introduction In automotive Body-in-White (BIW), automotive components, and new energy vehicle structural manufacturing, stud welding is widely used for applications such as cable harness fixing, heat shield installation, interior component mounting, and structural part assembly. However, in actual production, issues such as poor weld integrity, porosity, slag inclusion, and incomplete fusion remain key factors affecting stud welding quality stability. In severe cases, these defects can reduce stud strength and even cause stud detachment, affecting downstream assembly processes and product reliability. Based on stud welding principles and practical industrial applications, this article systematically analyzes the formation mechanisms, major causes, and engineering solutions for porosity and slag inclusion defects. 1. Formation Mechanism of Porosity and Slag Inclusion 1.1 Porosity Formation Mechanism: During the stud welding process, the high-temperature arc rapidly melts the welding area and forms a weld pool. If gases (such as H₂, CO, and N₂) inside the weld pool cannot escape before the molten metal solidifies, they will remain trapped inside the weld and form porosity. Porosity is mainly classified into: Surface porosity Internal porosity Among them, internal porosity is more difficult to detect and can reduce the effective strength of the welded joint. 1.2 Slag Inclusion Formation Mechanism: Slag inclusion refers to non-metallic impurities generated during the welding process that fail to escape in time and remain trapped inside the weld after solidification, forming defects. The main sources include: Oxides on the base material surface Oil contamination and foreign materials Coating residues Oxidation products generated during the welding process Slag inclusion reduces the effective bonding area of the weld and creates stress concentration areas, affecting weld joint reliability. 2. Six Root Causes of Porosity and Slag Inclusion 2.1 Workpiece Surface Contamination — The Most Common Cause Insufficient cleaning before welding is the primary cause of porosity and slag inclusion….
2026-07-21
Although defects such as weld nugget deviation and cold welds/incomplete fusion cannot be completely eliminated, their occurrence can be reduced to an extremely low level through systematic process control, real-time quality monitoring, and regular equipment maintenance. The following solutions focus on two critical defect areas — weld nugget deviation and cold welding/incomplete fusion — combining proven process optimization methods with advanced intelligent welding technologies. 1. Precise Control of Weld Nugget Deviation Weld nugget deviation is mainly caused by arc blow (magnetic arc deflection) and uneven heat dissipation conditions. 1.1 Eliminating Arc Blow — Prevention at the Source Symmetrical grounding (core measure) The ground connections should be positioned symmetrically on both sides of the welding location. This prevents uneven electromagnetic fields from deflecting the arc and is the most effective method for eliminating arc blow. Remove or ground nearby metal masses If large metal components, reinforcement plates, or conductive structures are located close to one side of the weld area, they should be removed or properly grounded to avoid magnetic field interference. Rotate the welding torch For manual stud welding, if arc deflection occurs toward one direction, rotating the torch handle by 90° can change the magnetic field distribution and improve arc stability. Control lift height Excessive lift height or missing ceramic ferrules can increase arc instability. Recommended lift height: General range: 1.0–1.6 mm Always use ceramic ferrules whenever possible to stabilize the arc. Figure: Symmetrical Grounding Configuration for Arc Blow Prevention Proper grounding layout plays a critical role in stabilizing the welding arc. Symmetrical grounding reduces magnetic field imbalance and prevents arc deflection, helping maintain consistent weld nugget positioning. 1.2 Optimizing Heat Distribution for Different Materials and Thicknesses Apply high-energy welding parameters Using a high current and short welding time (strong welding schedule) increases current density and reduces the influence…