 2026-09-07
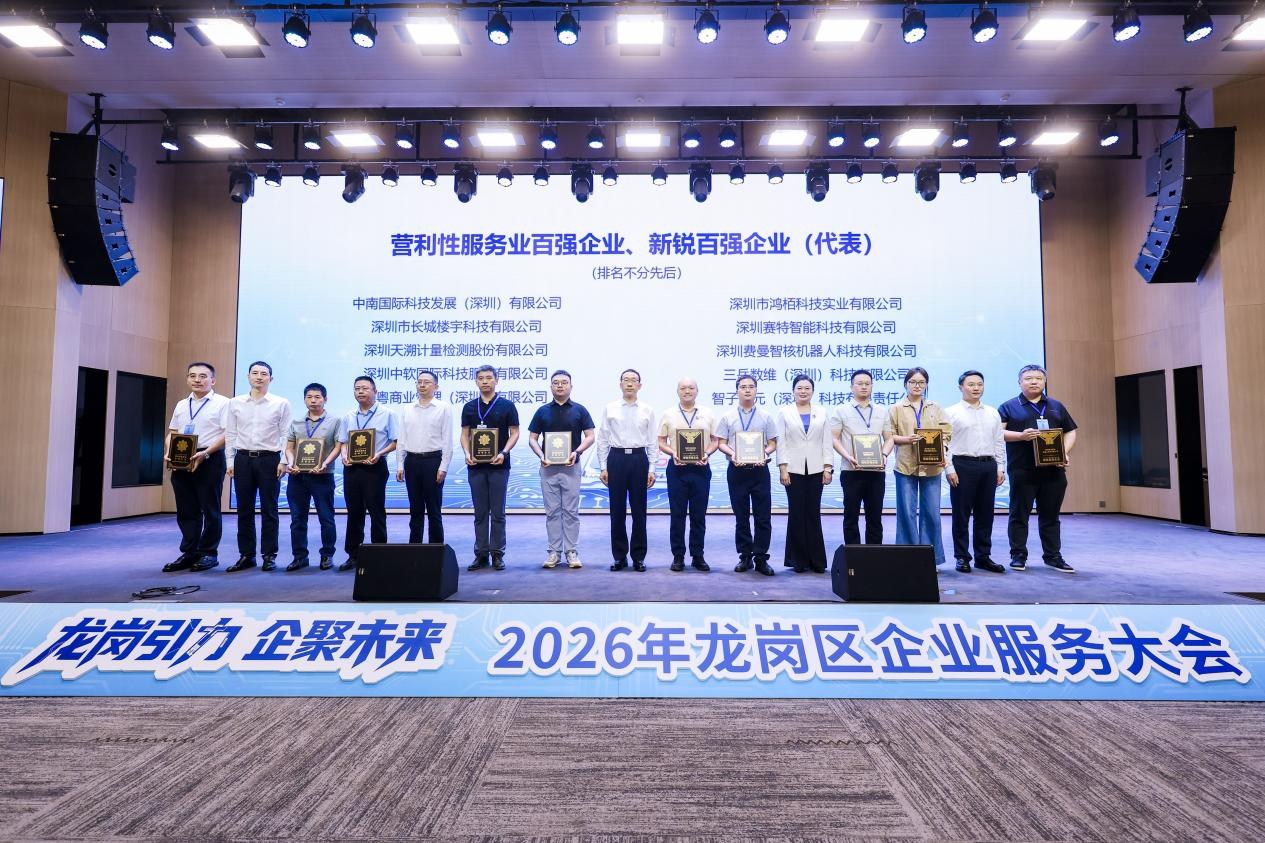
Shenzhen, China — September 2026 — Shenzhen Hongbai Technology Co., Ltd. has been recognized as one of the Top 100 Emerging Enterprises in Longgang District, following the announcement made at the 2026 Longgang Enterprise Service Conference. The conference was hosted by the CPC Longgang District Committee and the Longgang District Government. Hongbai Technology was selected for its strong innovation capabilities, solid technical expertise, and continued growth, marking another important recognition of the company’s development in Longgang and its more than 20 years of commitment to intelligent welding equipment. More Than 20 Years of Technology and Manufacturing Founded in 2003 and headquartered in Longgang District, Shenzhen, Hongbai Technology is a National High-Tech Enterprise and a National-Level Key “Little Giant” Enterprise, as well as a Guangdong Manufacturing Single Champion Enterprise and a standing council member of the China Welding Association. The company has also participated in national key scientific and technological research projects and National Torch Program projects. Hongbai Technology focuses on the R&D and manufacturing of intelligent equipment and customized industrial software, with capabilities covering the complete process from core technology development and precision manufacturing to system integration. With more than two decades of experience, the company has built particular expertise in automotive manufacturing and intelligent welding equipment, serving the evolving needs of modern manufacturing. Strong R&D and Engineering Capabilities Hongbai Technology currently has nearly 600 employees, with R&D personnel accounting for approximately 30% of its workforce. The company invests more than 15% of its annual sales revenue in R&D, continuously developing technologies for intelligent welding, automation, robotics, industrial software, and AI-enabled manufacturing. To date, Hongbai Technology has accumulated more than 200 patents and software copyrights across its domestic and international technology portfolio. The Guangdong Engineering Technology Research Center for Welding Equipment is also based at Hongbai Technology, further supporting the…
 2026-09-05
Why Monitor Penetration in Stud Welding? In stud welding, the result is not simply about whether the stud is attached to the workpiece. When the stud tip and workpiece surface are melted, sufficient fusion must be achieved to form a reliable joint. Insufficient fusion can affect joint strength, while excessive heat input may cause localized overheating or even burn-through when welding thin sheet metal. In conventional production, engineers typically control the process through parameters such as welding current, welding time, and lift height, followed by visual inspection and sampling-based destructive testing. But these methods do not always answer a more direct question: What actually happened to this individual stud during the weld? This is where the penetration monitoring function of the PIDS Series Stud Welding System comes into play. The system monitors the change in stud position before and after welding, calculates the corresponding penetration value, and provides the result on the operator interface after the weld is completed. Penetration therefore becomes a measurable process variable rather than something that can only be evaluated indirectly through post-weld inspection. 1. How Does PIDS Penetration Monitoring Work? 1.1 The Principle Is Measurement, Not Visual Inspection PIDS penetration monitoring does not rely on a camera to directly observe the molten pool after welding. Instead, it is based on the change in stud position before and after the welding cycle. Before welding begins, the system establishes the initial stud position as a reference. Once the arc is initiated, the stud tip and workpiece surface melt to form a molten pool. The stud then moves into the molten pool and the weld is completed. After welding, the system records the final stud position. The change between the initial and final positions is then used to calculate the corresponding penetration value. The process can be simplified…
 2026-09-01
1. Stud Welding in Sheet Metal Electrical Enclosure Manufacturing Stud welding is widely used for fastening applications in electrical enclosures, control cabinets, switchgear cabinets, distribution boxes, and other sheet metal structures. Compared with conventional nut welding, drilling and tapping, or mechanical fastening, stud welding allows a threaded stud or fastening element to be permanently attached directly to the sheet metal surface, reducing additional machining and assembly operations. Typical applications include grounding studs, mounting studs for circuit breakers and terminal blocks, busbar supports, cable management components, door hardware, and other internal cabinet components. In practical production, the selection of a sheet metal stud welding process depends mainly on sheet thickness, stud diameter, base material, required joint strength, surface condition, and the appearance requirements of the opposite side of the workpiece. For thin sheet metal electrical enclosures, minimizing distortion, discoloration, and visible marks on the reverse side can be particularly important. For structural components and grounding connections, weld strength and process consistency may take priority. Therefore, selecting stud welding equipment for electrical enclosures requires more than simply checking the welding current or stud diameter. The welding power source, stud welding gun, stud feeder, workholding system, and level of automation all need to be considered as part of the same process. 2. Capacitor Discharge and Drawn Arc Stud Welding 2.1 Capacitor Discharge Stud Welding Capacitor discharge (CD) stud welding stores electrical energy in capacitors and releases it over an extremely short welding cycle. Typical welding time is approximately 0.001–0.003 seconds, with peak current reaching approximately 5,000–10,000 A. Because the welding cycle is extremely short, heat input is concentrated around the weld area. This makes capacitor discharge stud welding particularly suitable for thin sheet metal and applications where backside appearance is important. Hongbai’s PFC Series capacitor discharge stud welding machines support stud diameters from…
 2026-08-26
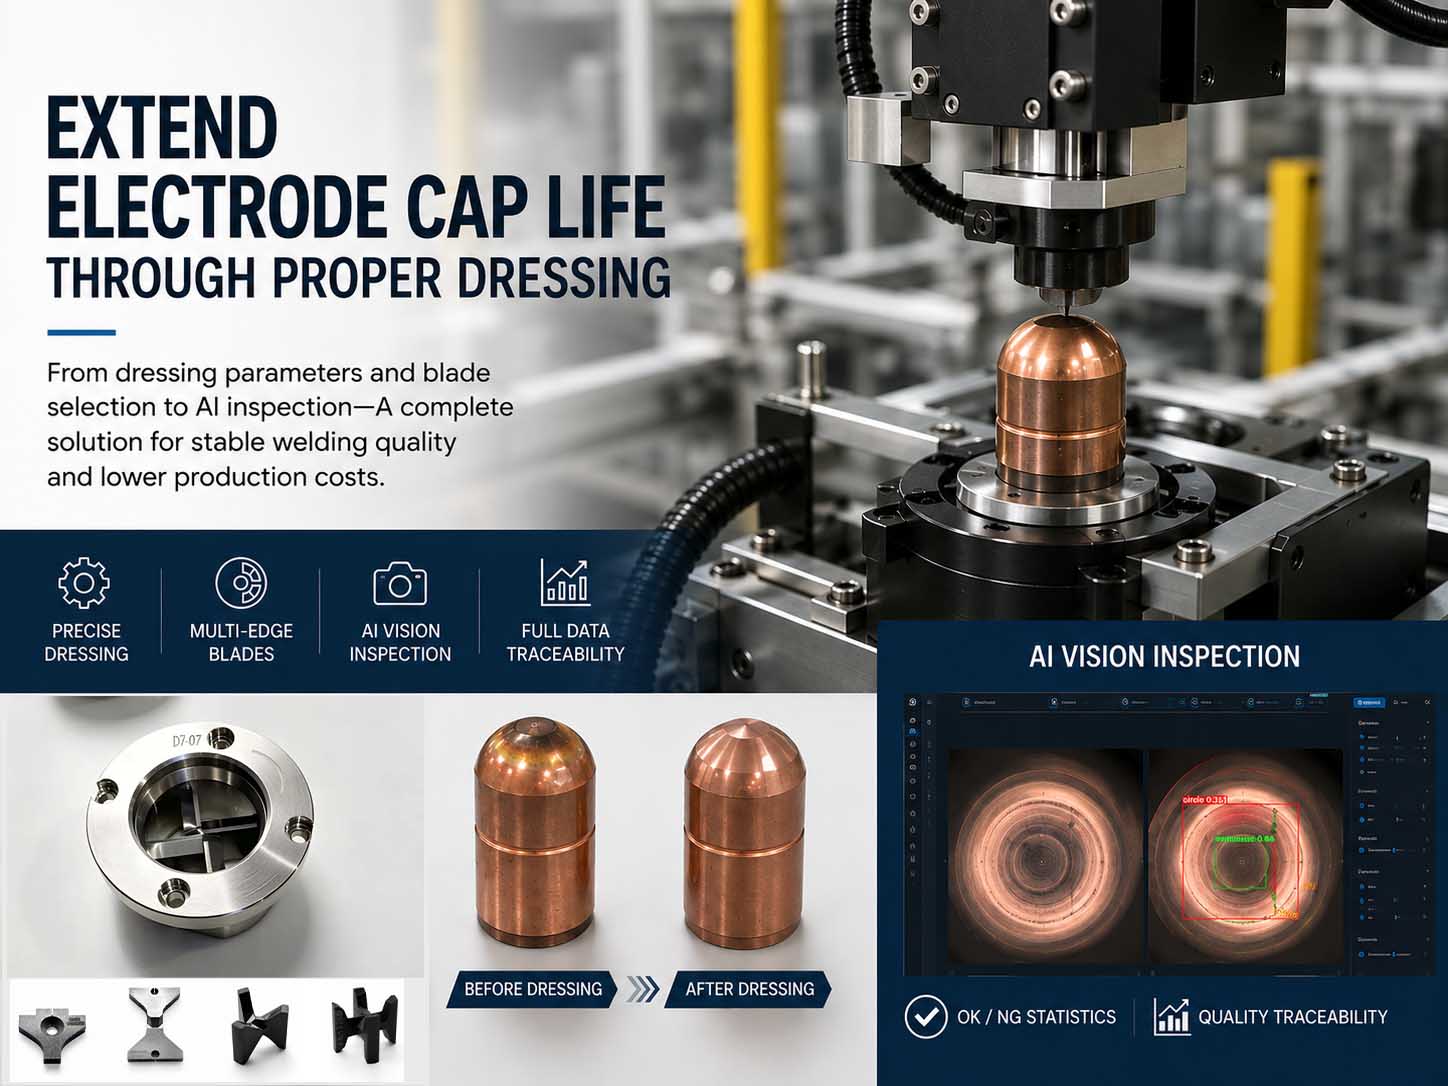
An electrode cap is a critical consumable component in resistance spot welding. It directly participates in the welding process and plays an important role in maintaining stable electrical and mechanical conditions at the weld interface. In automotive manufacturing, Body-in-White (BIW) production and other high-volume automated spot welding applications, the condition of the electrode cap can directly affect weld quality, process stability and production efficiency. As the number of welds increases, the working face of the electrode cap gradually becomes worn, deformed or contaminated. Copper pickup, surface marks and other irregularities may also develop during continuous welding. Electrode cap dressing is therefore used to remove the damaged surface layer and restore the required geometry and working condition of the electrode cap. However, electrode cap dressing is not simply a matter of removing as much material as possible.Insufficient dressing may leave damaged areas on the working face, while excessive dressing unnecessarily removes electrode material and reduces the number of effective dressing cycles available from a single electrode cap. Therefore, controlling the dressing amount, selecting the right dressing cutter, performing routine maintenance and using intelligent inspection to identify abnormalities are all important for extending electrode cap life. In practical production applications, electrode cap dressing performance can be systematically improved through four key areas. 1. Control the Dressing Amount to Avoid Excessive Material Removal The primary objective of electrode cap dressing is to remove damaged material and restore the required working face—not to remove more material than necessary. If the dressing amount is insufficient, defects generated during welding may remain on the electrode face, including black marks, raised areas, localized wear and uneven surfaces. These conditions can alter current density and electrode force distribution, potentially affecting weld consistency. On the other hand, excessive dressing removes a larger amount of otherwise usable electrode material. This…
 2026-08-22
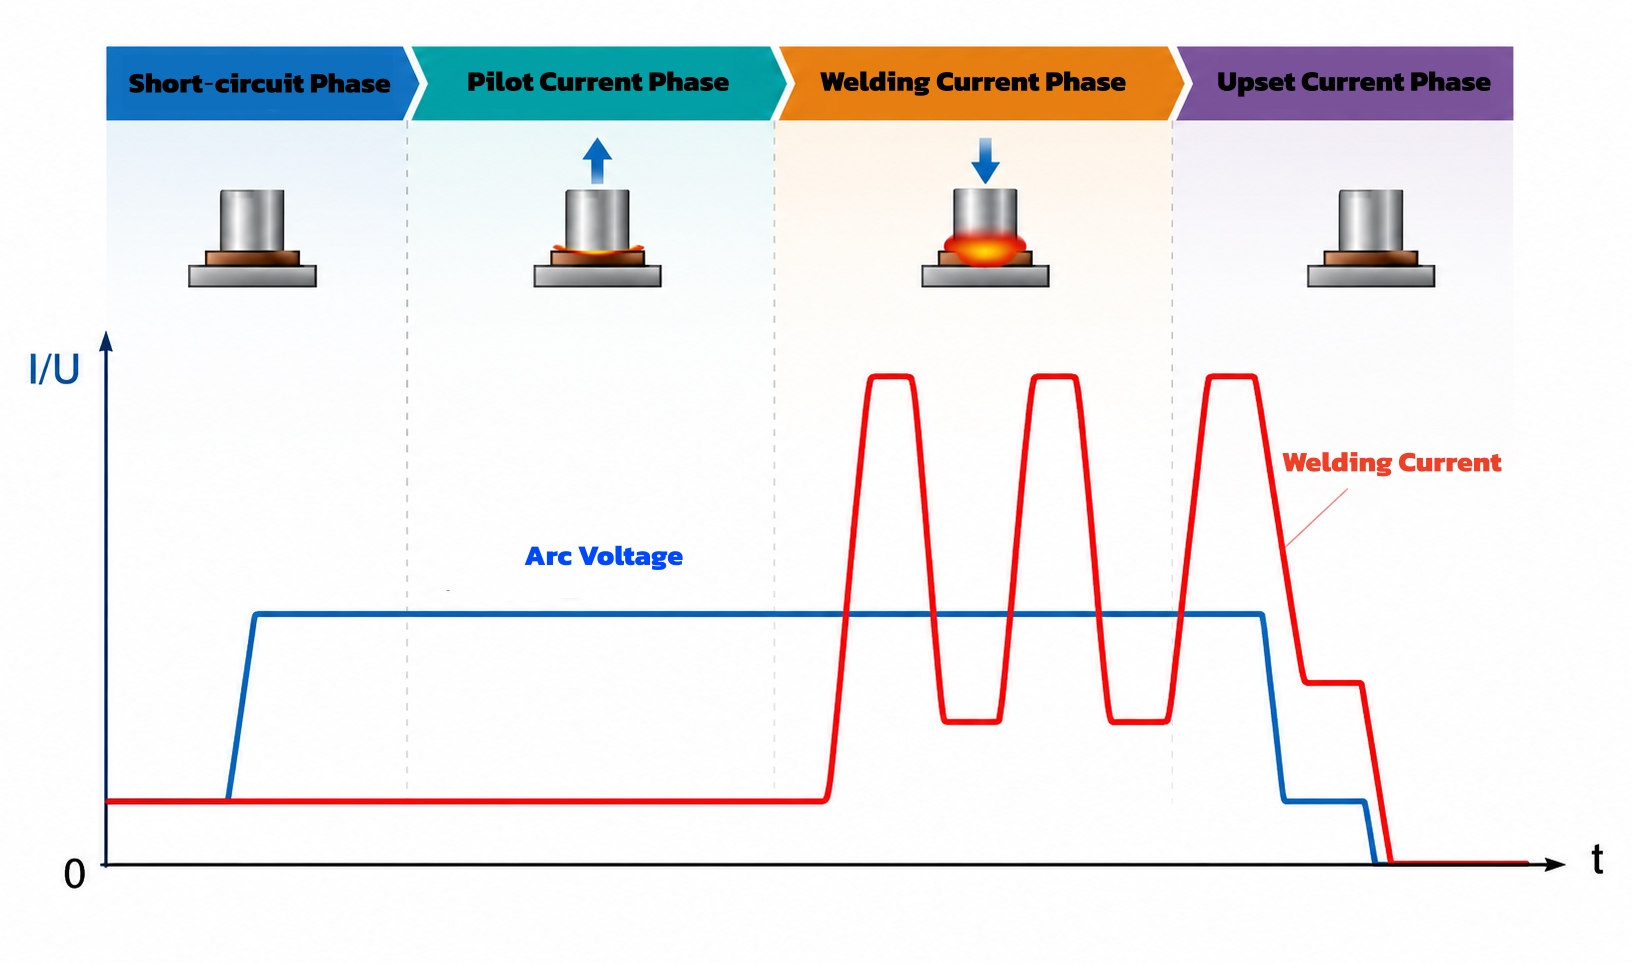
1. Start with the Application: How to Choose the Right Stud Welding Machine? As automotive manufacturing, sheet metal fabrication, appliance production, machinery manufacturing, and industrial automation continue to evolve, stud welding is moving from traditional manual operations toward automated, robotic, and digital production. For manufacturers, selecting a stud welding machine is no longer simply about comparing maximum welding current. Stud diameter, workpiece material, sheet thickness, required joint strength, production cycle time, and automation level all influence the final equipment selection. As a company specializing in intelligent welding equipment and industrial automation, Hongbai Technology has been developing stud welding technology since 2003. Its product portfolio covers capacitor discharge stud welding, short-cycle drawn arc welding, AC/DC stud welding, CNC automatic stud welding platforms, and robotic stud welding systems. Depending on the material, stud specification, and production method, Hongbai can provide complete solutions covering welding power sources, servo welding guns, automatic stud feeders, robots, and CNC platforms. Before selecting a machine, therefore, the first question should be: What type of stud welding process does your application actually require? 2. Choose the Welding Process Before Choosing the Machine Different stud welding processes operate differently and therefore have different requirements for the welding power source and welding gun. The two main processes used in industrial production are capacitor discharge stud welding and drawn arc stud welding. Capacitor discharge stud welding uses stored capacitor energy to complete the weld within an extremely short period, typically around 1–3 ms. This results in low heat input and minimal thermal impact on thin sheets. It is particularly suitable for small-diameter studs, typically 3–8 mm, thin sheet applications, and components where backside deformation must be minimized. Drawn arc stud welding, on the other hand, uses the welding gun to lift the stud and create an arc between the stud and…
 2026-08-19
In July 2026, at the AMTS Shanghai International Automotive Manufacturing Technology & Material Show, Hongbai Technology made the global debut of its fully self-developed AI foundation-model-powered stud welding quality inspection system. It is also the world’s first quality management system integrating an AI foundation model specifically for stud welding applications. As AI foundation models rapidly transform industries worldwide, Hongbai Technology is bringing this transformation to the welding industry. After six generations of welding technology evolution, the company has consistently focused on the integration of data, algorithms, and real-world industrial scenarios, while addressing four fundamental challenges in industrial AI. Through the dual revolution of “Welding + AI,” Hongbai Technology is pioneering a new paradigm for stud welding quality management—moving from experience-driven quality control to data- and algorithm-driven intelligence. 1. Industry Challenges: Four Limitations of Traditional Quality Inspection 1.1 Fragmented and Heterogeneous Data In high-volume stud welding production, traditional quality management faces a series of systemic challenges. Fragmented and heterogeneous data: Quality records are often scattered across paper documents, PowerPoint files, Excel spreadsheets, welding equipment, and other systems, making data integration time-consuming and inefficient. 1.2 Slow Problem Detection and Response Quality issues may take up to four hours to be detected under periodic inspection. Once identified, the escalation and feedback process may require another 1–2 hours, while problem resolution can take up to 3.5 hours. In addition, compiling daily quality inspection reports can consume approximately 2.25 hours of labor every day. For high-volume automotive production, such delays increase the risk of quality issues escaping downstream and can lead to additional rework and production costs. 1.3 Manufacturing Knowledge Is Difficult to Capture and Reuse Root cause identification and corrective action often depend heavily on the experience of individual engineers and technicians. When critical welding knowledge remains primarily within individual experts, it becomes difficult…
 2026-08-11
In the demanding environment of automotive Body-in-White (BIW) welding, electrode cap dressing blades may appear small, but they play a critical role in determining weld spot quality, electrode cap service life, and overall production cost. Behind a seemingly simple blade lies a complete chain of engineering expertise, including material science, precision manufacturing, and strict quality management. With decades of experience in welding equipment development, Shenzhen Hongbai Technology Co., Ltd. has successfully transformed its independently developed electrode cap dressing blades from ordinary consumable components into precision-engineered products integrating advanced structural design, high-accuracy manufacturing processes, and international certification standards. 1. Design Philosophy: A Fundamental Shift from “Cutting” to “Dressing” Traditional electrode cap dressing is essentially a cutting process, where sharp cutting edges forcibly remove the copper-aluminum alloy layer accumulated on the electrode cap surface. Although this method is straightforward, it has two major limitations: High material removal rate (approximately 0.08 mm per dressing cycle) Short blade service life (only around 8,000–12,000 dressing cycles for single-edge blades) Hongbai’s dressing blade design achieves a breakthrough by redefining the fundamental dressing principle. 1.1 Multi-Edge Structure: From Single Cutting to Multi-Stage Dressing The core innovation of Hongbai dressing blades lies in the multi-edge structure. Currently, Hongbai provides four blade configurations. Taking the four-edge blade as an example, its four cutting edges are arranged at 90-degree intervals. During the dressing process, multiple edges work simultaneously, distributing cutting forces across several contact points. This reduces the material removal amount per dressing cycle to only 0.01–0.035 mm, bringing the process closer to precision dressing rather than conventional cutting. The direct benefits include: Reduced electrode cap material consumption Extended electrode cap service life Increased welding capacity from approximately 3,000 weld spots to 6,000 weld spots per pair of electrode caps 1.2 Four-Edge Right-Angle Design: 90° Geometry and 0.01 mm Dressing…
 2026-08-10
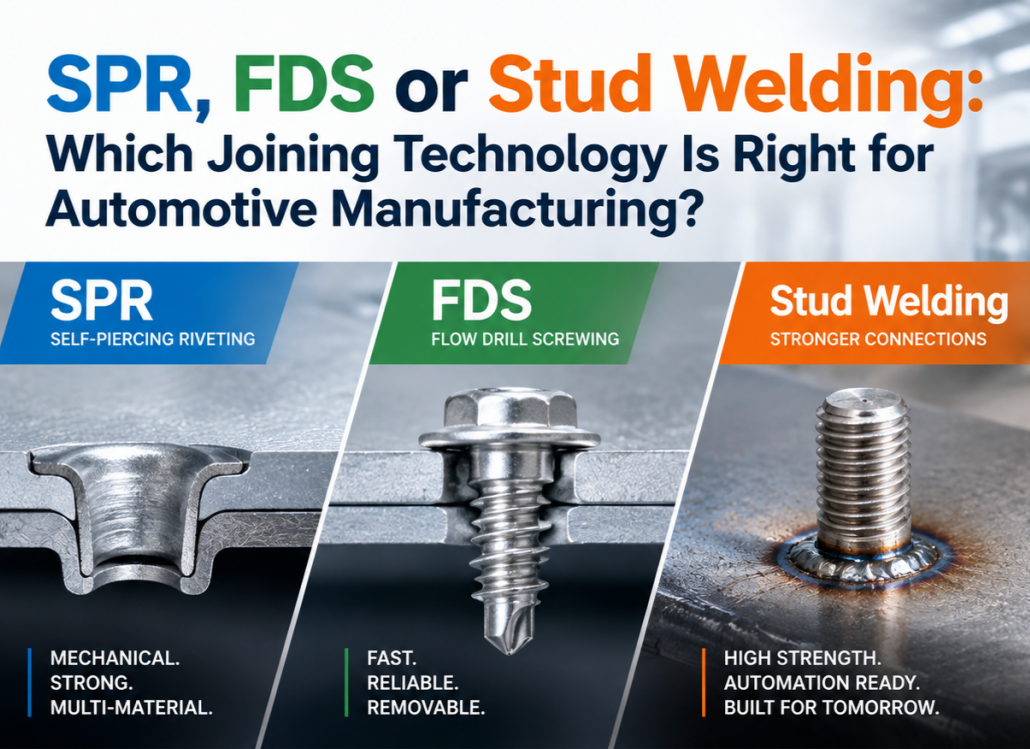
Introduction: The Evolution of Joining Technology in Modern Manufacturing For decades, resistance spot welding and traditional welding processes have been widely used in automotive manufacturing and industrial production. However, the rapid development of electric vehicles (EVs), lightweight structures, and multi-material applications has created new challenges for joining technologies. Modern manufacturing is no longer limited to single-material structures. Increasingly, manufacturers are working with combinations of: High-strength steel (AHSS) Aluminum alloys Galvanized steel Composite materials Multi-layer structures These materials provide significant advantages in weight reduction, energy efficiency, and product performance. However, they also introduce new challenges, including: Material compatibility issues Welding deformation Porosity and cracking risks Difficult access in complex structures Higher requirements for automation and quality monitoring For example, aluminum alloys have high thermal conductivity and a stable oxide layer on the surface, making traditional fusion welding more challenging. Problems such as unstable arc initiation, heat distortion, and welding defects can affect connection reliability. In addition, joining dissimilar materials such as steel and aluminum remains difficult due to differences in melting temperature, thermal expansion, and metallurgical properties. As a result, advanced joining technologies such as Stud Welding, SPR (Self-Piercing Riveting), and FDS (Flow Drill Screwing) have become increasingly important solutions for modern manufacturing. These technologies are not replacements for each other. Instead, each technology provides unique advantages for different material combinations, structural designs, and application requirements. 1. Stud Welding: A Reliable Solution for Functional Fastening Stud welding is a process that permanently joins a metal stud to a workpiece through an arc welding process. During welding, an arc is generated between the stud and the base material. After the contact surface melts, pressure is applied to complete the weld, creating a strong metallurgical connection. Unlike traditional welding methods that mainly join metal components together, stud welding creates an integrated fastening point…
 2026-08-06
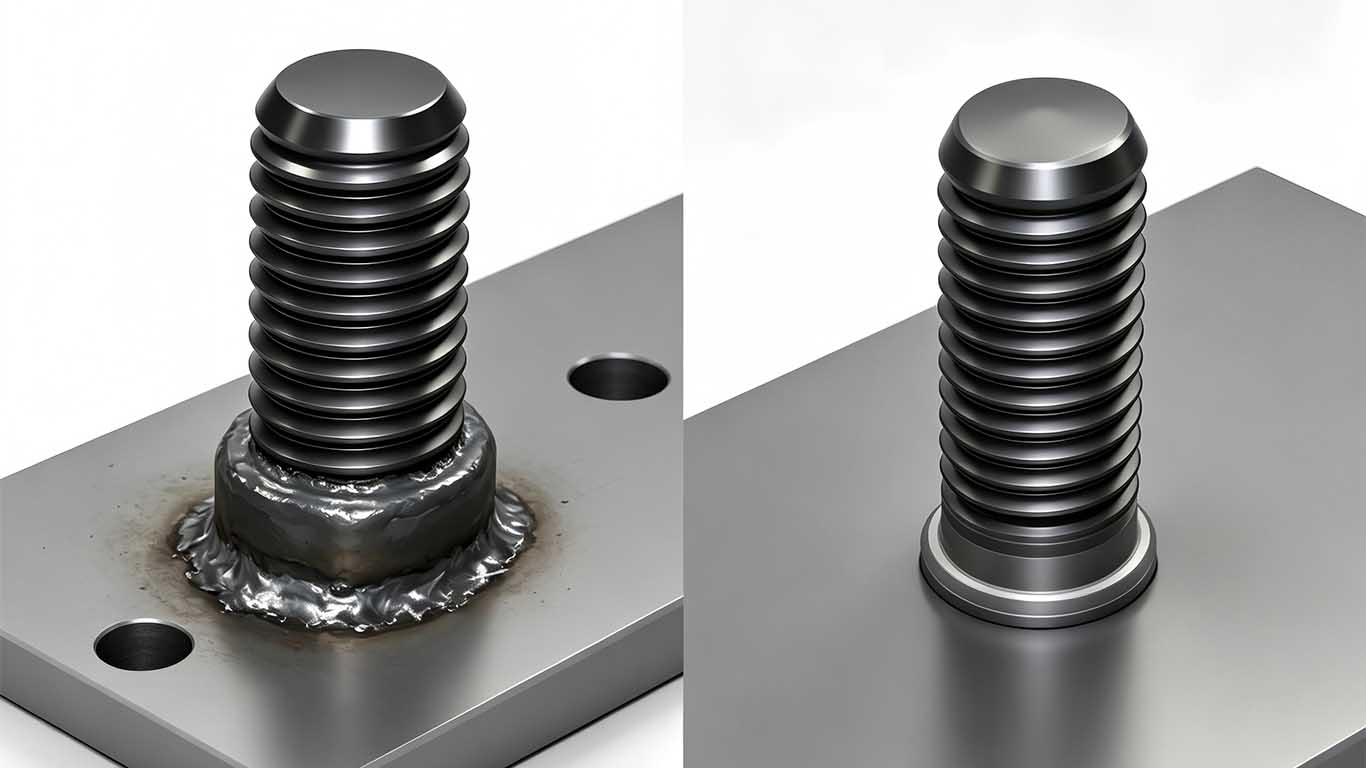
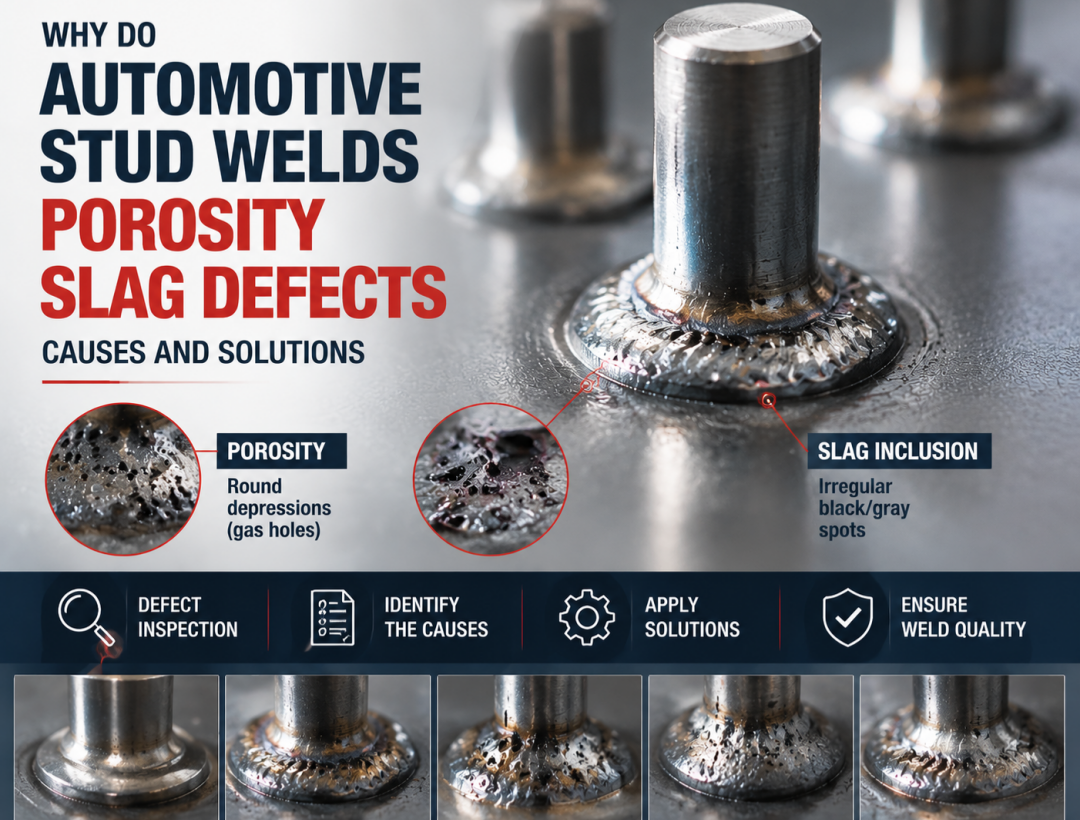
Introduction In automotive Body-in-White (BIW), automotive components, and new energy vehicle structural manufacturing, stud welding is widely used for applications such as cable harness fixing, heat shield installation, interior component mounting, and structural part assembly. However, in actual production, issues such as poor weld integrity, porosity, slag inclusion, and incomplete fusion remain key factors affecting stud welding quality stability. In severe cases, these defects can reduce stud strength and even cause stud detachment, affecting downstream assembly processes and product reliability. Based on stud welding principles and practical industrial applications, this article systematically analyzes the formation mechanisms, major causes, and engineering solutions for porosity and slag inclusion defects. 1. Formation Mechanism of Porosity and Slag Inclusion 1.1 Porosity Formation Mechanism: During the stud welding process, the high-temperature arc rapidly melts the welding area and forms a weld pool. If gases (such as H₂, CO, and N₂) inside the weld pool cannot escape before the molten metal solidifies, they will remain trapped inside the weld and form porosity. Porosity is mainly classified into: Surface porosity Internal porosity Among them, internal porosity is more difficult to detect and can reduce the effective strength of the welded joint. 1.2 Slag Inclusion Formation Mechanism: Slag inclusion refers to non-metallic impurities generated during the welding process that fail to escape in time and remain trapped inside the weld after solidification, forming defects. The main sources include: Oxides on the base material surface Oil contamination and foreign materials Coating residues Oxidation products generated during the welding process Slag inclusion reduces the effective bonding area of the weld and creates stress concentration areas, affecting weld joint reliability. 2. Six Root Causes of Porosity and Slag Inclusion 2.1 Workpiece Surface Contamination — The Most Common Cause Insufficient cleaning before welding is the primary cause of porosity and slag inclusion….
 2026-07-21
Although defects such as weld nugget deviation and cold welds/incomplete fusion cannot be completely eliminated, their occurrence can be reduced to an extremely low level through systematic process control, real-time quality monitoring, and regular equipment maintenance. The following solutions focus on two critical defect areas — weld nugget deviation and cold welding/incomplete fusion — combining proven process optimization methods with advanced intelligent welding technologies. 1. Precise Control of Weld Nugget Deviation Weld nugget deviation is mainly caused by arc blow (magnetic arc deflection) and uneven heat dissipation conditions. 1.1 Eliminating Arc Blow — Prevention at the Source Symmetrical grounding (core measure) The ground connections should be positioned symmetrically on both sides of the welding location. This prevents uneven electromagnetic fields from deflecting the arc and is the most effective method for eliminating arc blow. Remove or ground nearby metal masses If large metal components, reinforcement plates, or conductive structures are located close to one side of the weld area, they should be removed or properly grounded to avoid magnetic field interference. Rotate the welding torch For manual stud welding, if arc deflection occurs toward one direction, rotating the torch handle by 90° can change the magnetic field distribution and improve arc stability. Control lift height Excessive lift height or missing ceramic ferrules can increase arc instability. Recommended lift height: General range: 1.0–1.6 mm Always use ceramic ferrules whenever possible to stabilize the arc. Figure: Symmetrical Grounding Configuration for Arc Blow Prevention Proper grounding layout plays a critical role in stabilizing the welding arc. Symmetrical grounding reduces magnetic field imbalance and prevents arc deflection, helping maintain consistent weld nugget positioning. 1.2 Optimizing Heat Distribution for Different Materials and Thicknesses Apply high-energy welding parameters Using a high current and short welding time (strong welding schedule) increases current density and reduces the influence…
 2026-07-16
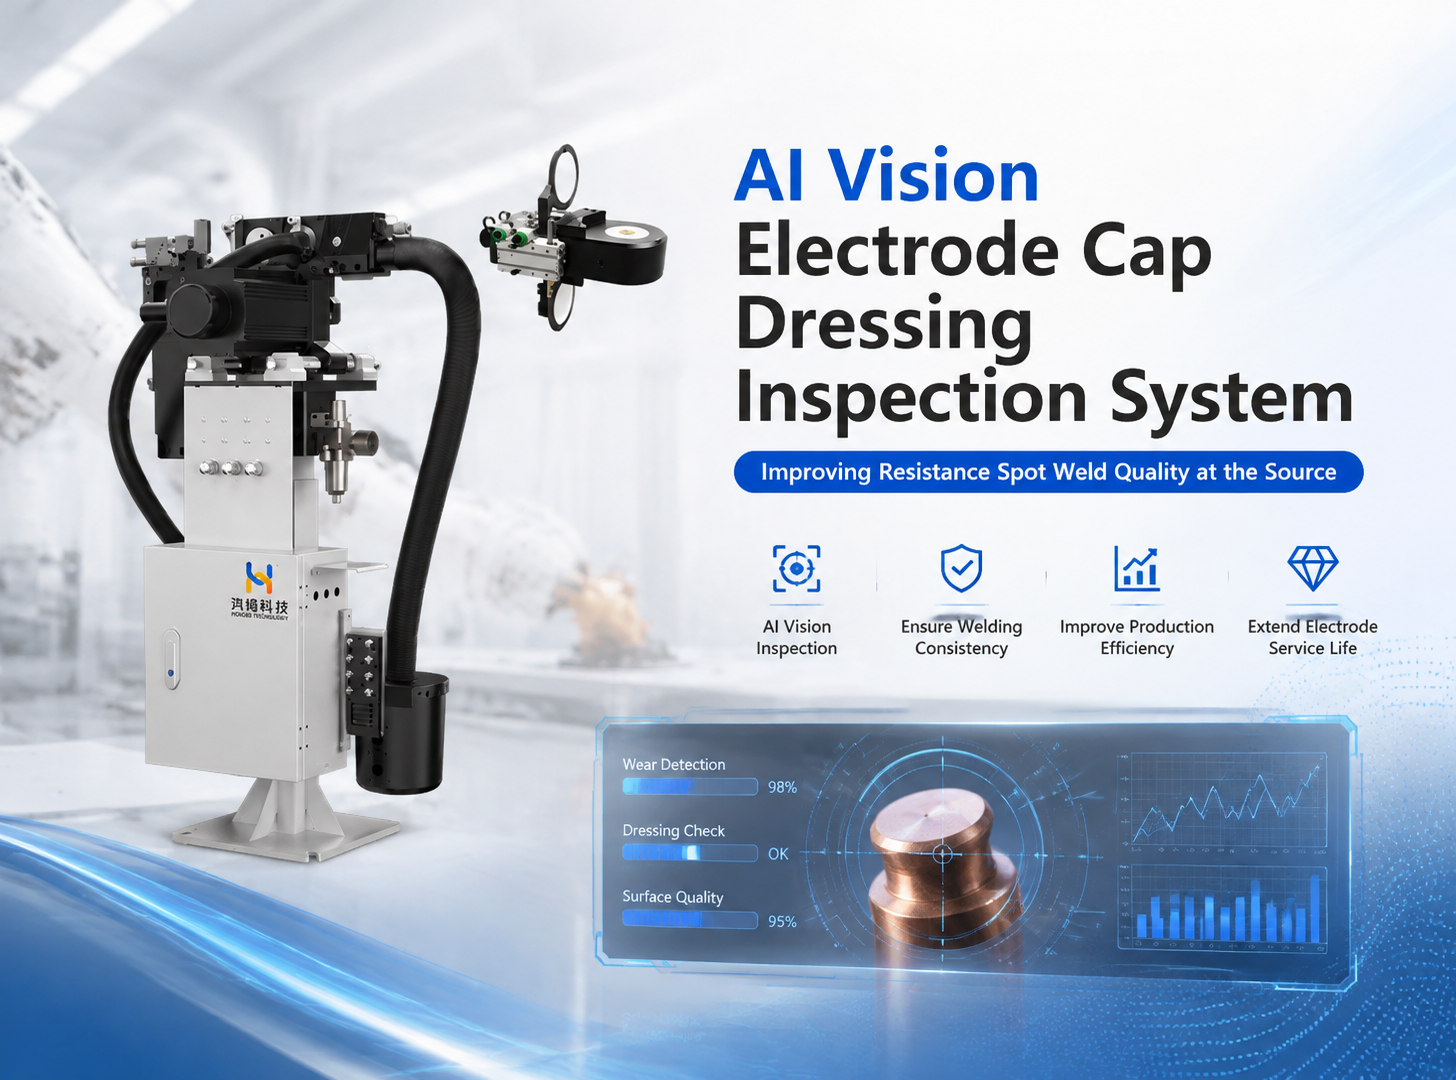
In automotive Body-in-White (BIW) production, resistance spot weld quality has a direct impact on vehicle structural integrity, safety, and durability. When investigating weld defects, manufacturers often focus on welding current, electrode force, and weld time. However, one critical factor affecting weld consistency is frequently overlooked—the condition of the electrode cap. Field experience has shown that inconsistent electrode cap dressing quality is one of the major causes of expulsion, undersized weld nuggets, weak welds, and poor weld consistency. As smart manufacturing continues to evolve, traditional maintenance methods based on manual inspection or fixed dressing intervals can no longer meet the requirements of high-speed automated production. AI-powered machine vision is rapidly becoming a new standard for resistance spot welding quality control. Why Is Electrode Cap Dressing So Important? The electrode cap directly influences current distribution and the electrical contact condition during resistance spot welding. After dressing, defects such as: • Off-center electrode face • Out-of-round electrode face • Copper pickup • Pits or raised surfaces • Incomplete or uneven dressing may result in: • Uneven current density • Inconsistent weld nugget size • Increased weld expulsion • Reduced weld strength • Shortened electrode life Therefore, electrode cap dressing quality affects not only electrode service life, but also the stability and consistency of every weld. Challenges with Conventional Electrode Dressing Many welding lines still rely on traditional electrode maintenance methods, including: • Dressing after a fixed number of welds • Manual visual inspection • Scheduled electrode cap replacement These methods present several limitations: • Inspection results depend heavily on operator experience. • Small surface defects are difficult to detect. • Premature dressing increases consumable costs, while delayed dressing compromises weld quality. • Lack of digital records makes root cause analysis and quality traceability difficult. For today’s high-volume automated welding lines, these approaches are…
 2026-06-25
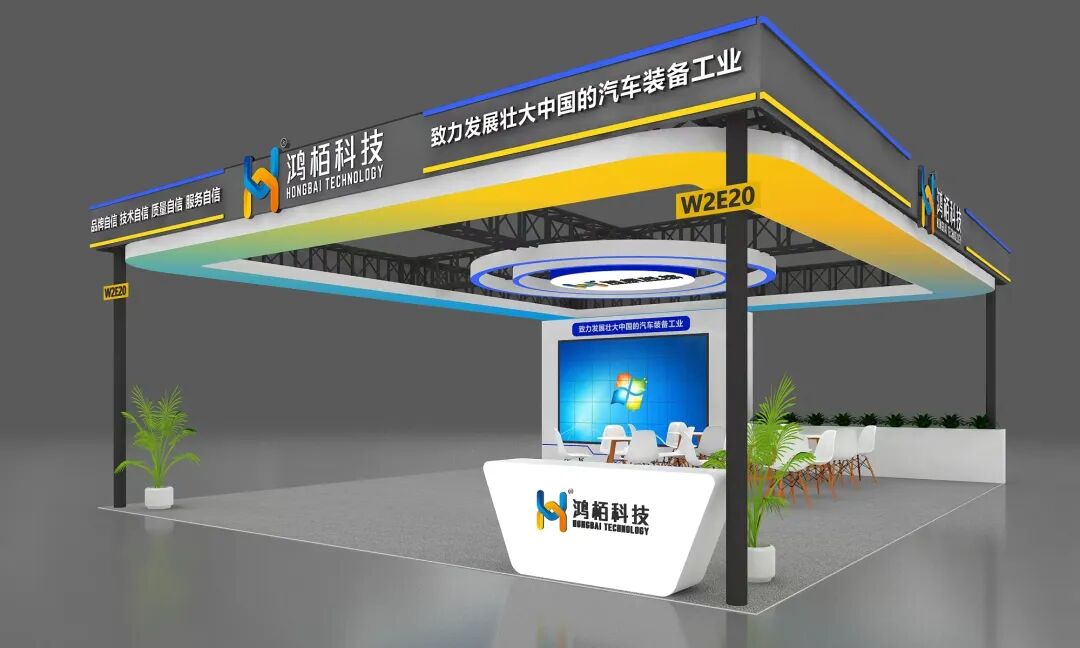
Date: July 8–10, 2026 Location: Shanghai New International Expo Centre Booth: W2‑E20 At AMTS 2026, Hongbai Technology demonstrates how closed‑loop welding solutions are transforming automotive manufacturing. From robotic stud welding to AI‑powered tip dressing, our 20 years of expertise come alive at Booth W2‑E20. We don’t just build machines — we build data‑driven quality assurance for every weld. Robotic Stud Welding: HEAS 5th‑Generation The HEAS robotic stud welding system is engineered for today’s toughest materials: aluminum car bodies, high‑strength steel, and ultra‑thin sheet metal. 0.34 ms current rise time ensures precise heat control 1 TB of full‑process data analyzed by our AI welding quality system One machine handles AC/DC for both steel and aluminum 4G/5G remote diagnostics and group control enabled One of the show’s biggest highlights: Hongbai Technology’s upgraded spot welding gun, paired with the HBXMQ‑003‑AOI dressing & changing unit featuring an AI vision inspection module, is deeply integrated with servo weld guns and FANUC robots to form a complete “Dressing – Inspection – Changing – Welding” closed‑loop workstation. Fits C‑type and X‑type welding guns 0.01 mm AI vision detects 11 electrode cap defects automatically Servo‑driven dress‑and‑change cycle in only 6 seconds Live demo: Watch dynamic tip dressing, real‑time visual inspection, and automated cap change Tip Dressing Machines for Every Production Line Hongbai offers a full range of tip dressers — from manual to fully automatic. Model Best for HBXMQ‑005 Handheld pneumatic, confined spaces HBXMQ‑001 Fixed motor‑driven, with copper dust collection HBXMQ‑002 Swing‑arm, ideal for robotic spot welding guns HBXMQ‑009 Single‑side automated dressing & changing HBXMQ‑007 Electrode cap removal, multi‑protocol All units use carbide‑coated blades and support IO, Profinet, Profibus. PIDS Semi‑Automatic Stud Welding Proven with FAW‑Volkswagen, BYD, and Tesla, the PIDS series delivers reliable semi‑automatic stud welding for flexible production. 1 A current accuracy via DSP digital control Linear motor lift with grating closed‑loop control 5 weld gun interfaces — one unit replaces five machines HBIES Servo Electric Cylinders A high‑performance domestic alternative, the HBIES servo electric cylinder uses a planetary roller screw for superior stiffness and life. 10 kN continuous thrust…
Others |
|
| Other uncategorized cookies are those that are being analyzed and have not been classified into a category as yet. | |
Necessary |
Necessary |
| Necessary cookies are absolutely essential for the website to function properly. These cookies ensure basic functionalities and security features of the website, anonymously. | |
Advertisement |
Necessary |
| Advertisement cookies are used to provide visitors with relevant ads and marketing campaigns. These cookies track visitors across websites and collect information to provide customized ads. | |
Analytics |
|
| Analytical cookies are used to understand how visitors interact with the website. These cookies help provide information on metrics the number of visitors, bounce rate, traffic source, etc. | |
Functional |
|
| Functional cookies help to perform certain functionalities like sharing the content of the website on social media platforms, collect feedbacks, and other third-party features. | |
Performance |
|
| Performance cookies are used to understand and analyze the key performance indexes of the website which helps in delivering a better user experience for the visitors. | |
This website uses cookies to improve your experience while you navigate through the website. Out of these, the cookies that are categorized as necessary are stored on your browser as they are essential for the working of basic functionalities of the website. We also use third-party cookies that help us analyze and understand how you use this website. These cookies will be stored in your browser only with your consent. You also have the option to opt-out of these cookies.